For the Elazığ factory of one of the world's largest
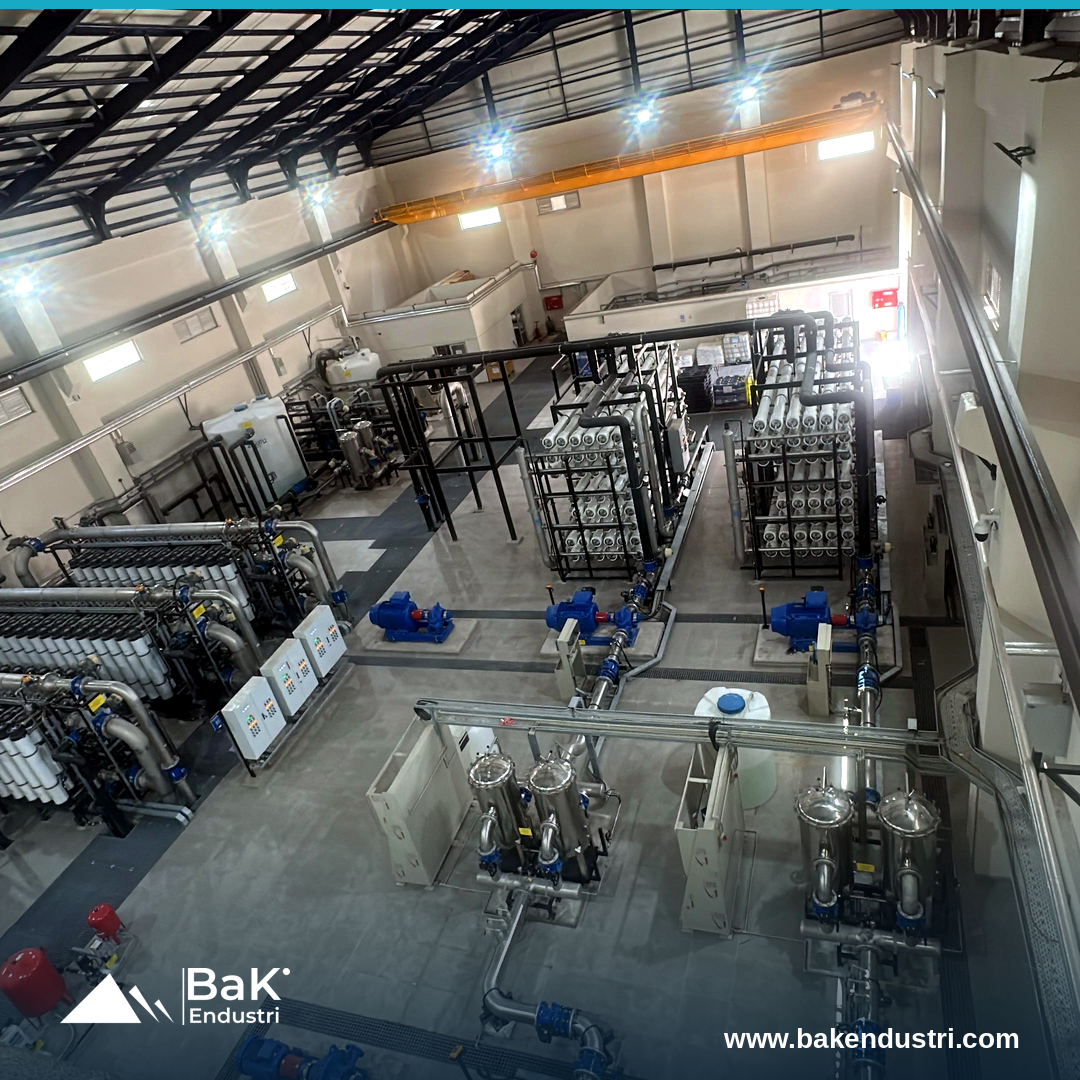
soft-drink brands, we built a turnkey water treatment plant to produce the
high-grade process water that forms the basis of product quality — meeting the
food sector's strictest hygiene and quality standards while supporting the
customer's water-efficiency goals.
The challenge: In beverage production — especially products
with a standardized formula — the water's taste, odor, and mineral balance
directly shape the final product. The goal: water that fully removes raw-water
variability, is 100% microbiologically safe, and is always to the same
standard.
The solution — a 2×95 m³/h, food-grade hygienic plant:
·
Multi-stage treatment:
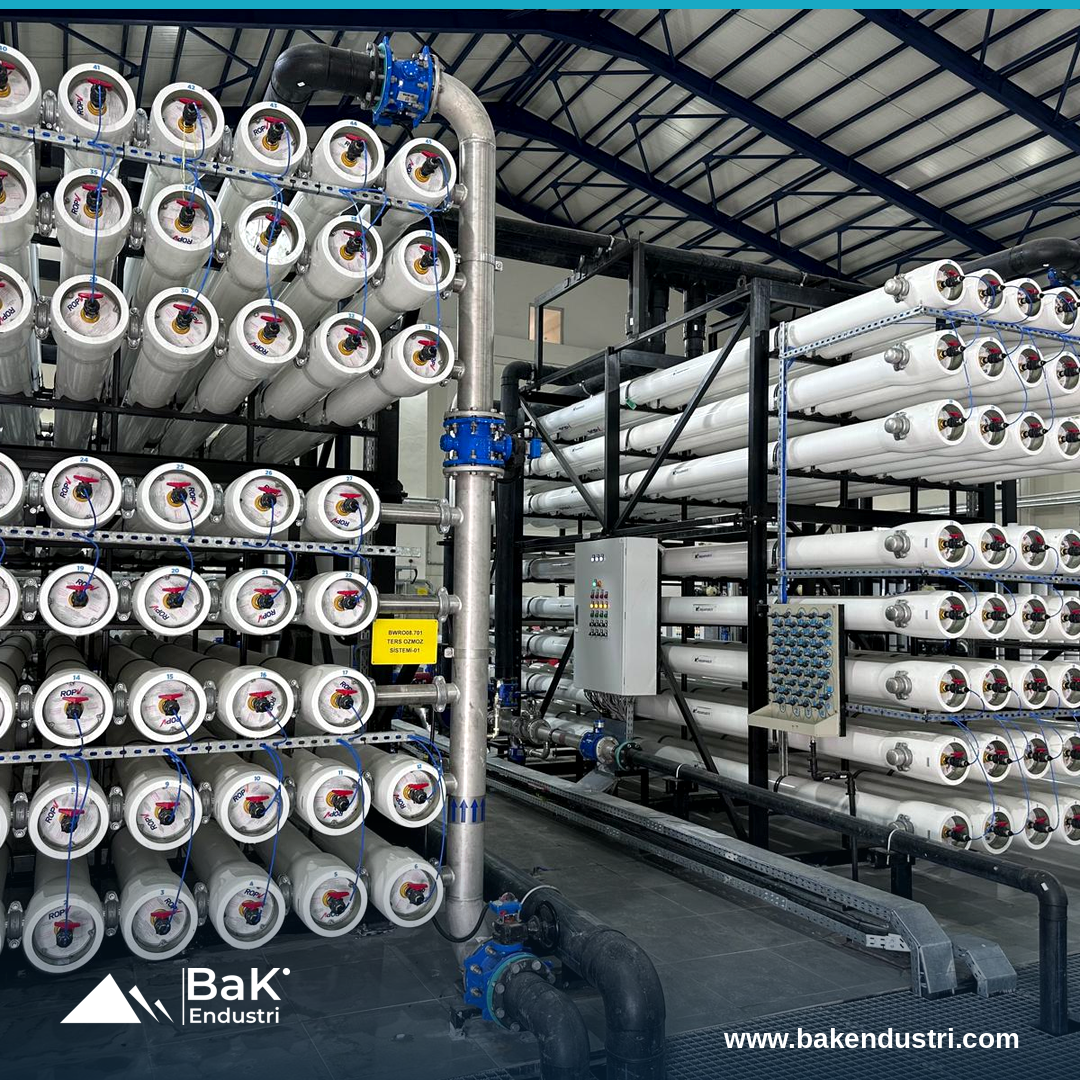
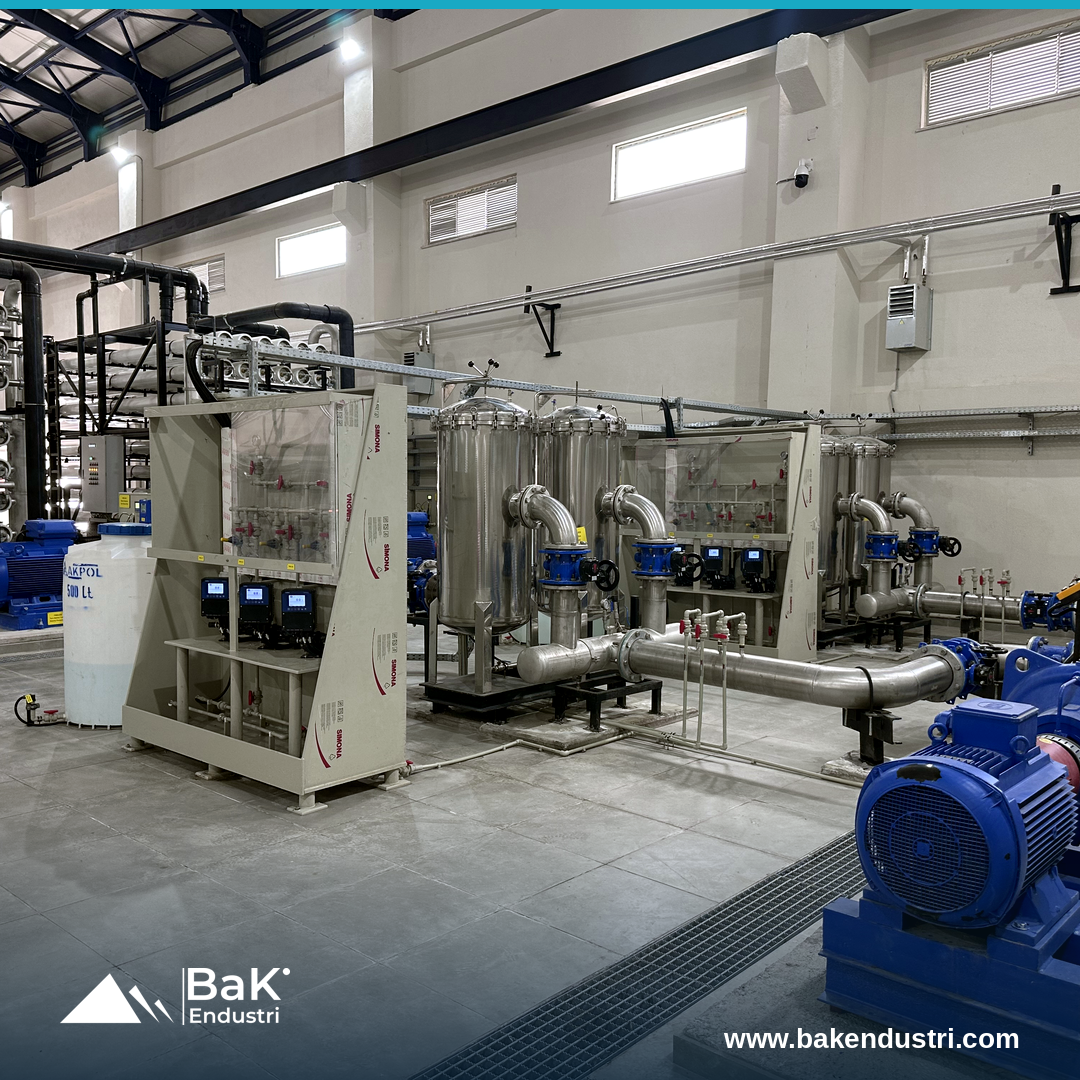
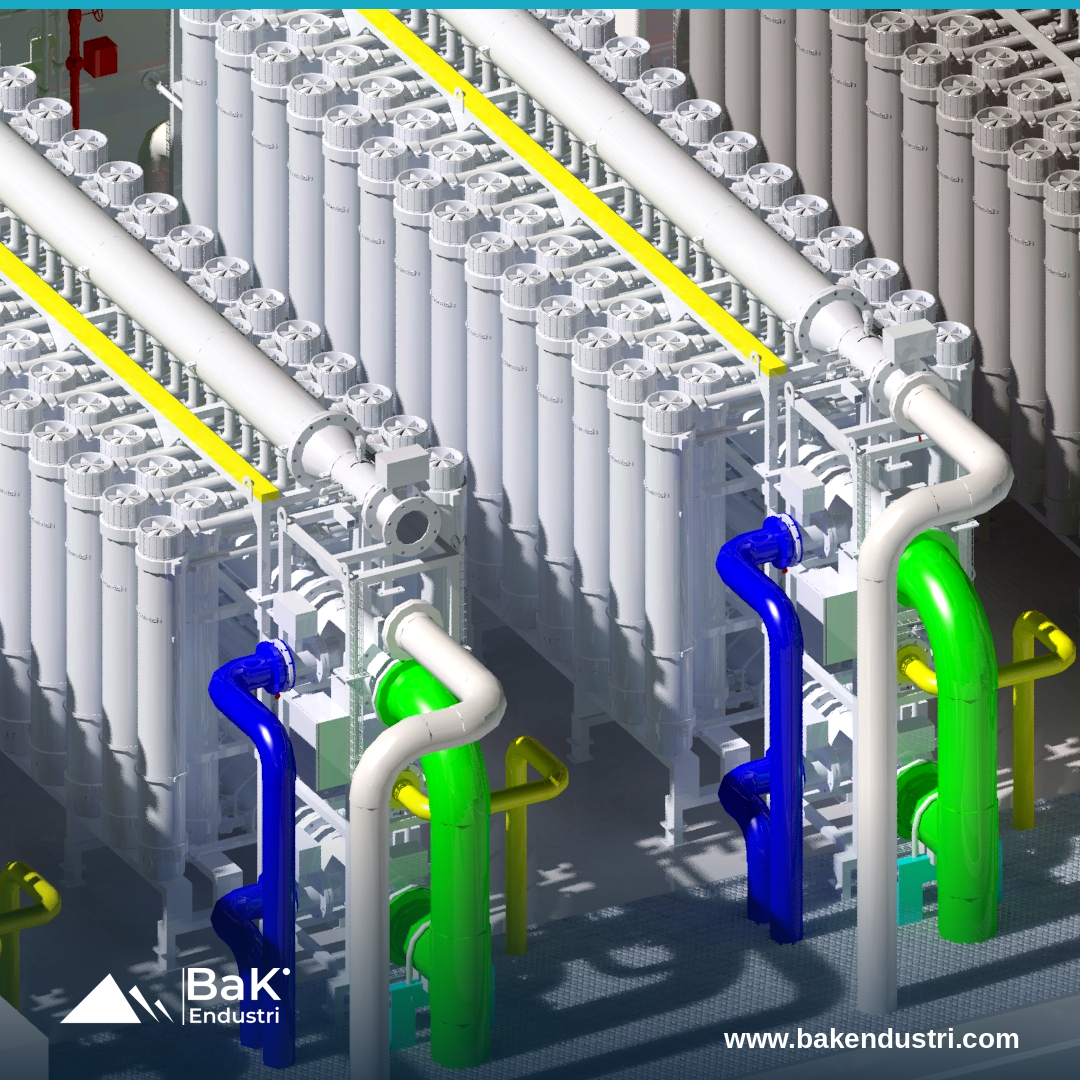
Ultrafiltration (UF) → Activated Carbon → parallel Reverse Osmosis (RO) and Nanofiltration (NF) lines (blended for mineral balance) for high efficiency and minimal water loss
·
UV disinfection +
steam-sterilizable activated carbon for full microbiological protection
·
All piping in 316L
food-grade stainless steel
·
Integrated CIP
(Cleaning-In-Place) for continuous hygiene
The result: uninterrupted first-class water for
internationally certified products; lower water consumption supporting
sustainability; and production continuity secured by a fully automatic,
hygienic design.